Solving the World’s Toughest CFD Problems

Sand Core Making Workspace

Workspace Overview

Increasing demands on casting quality, along with the trend toward thin-walled structures for high-performance components, have placed stricter requirements on sand core quality while increasing geometric complexity. The Sand Core Making Workspace provides users with an easy-to-use tool for modeling the shooting and hardening of sand cores. Users will be able to model the shooting of a wide range of sand and binder combinations to predict how a core box fills, locate regions where inadequate filling occurs, and then place and size air vents to improve filling in those regions. All current core hardening processes can be modeled, including cold box, hot box, and inorganic processes. Shooting characteristics such as sand density distribution and air flow can be readily visualized.

Workspace Highlights

  • Granular flow air/sand characterization of sand fill
  • Pressure driven sand non-fill prediction analysis
  • Database includes all permutations of organic (hot and cold box) and inorganic binders for hardening

Sand Core Making Playlist
8 Videos
Description

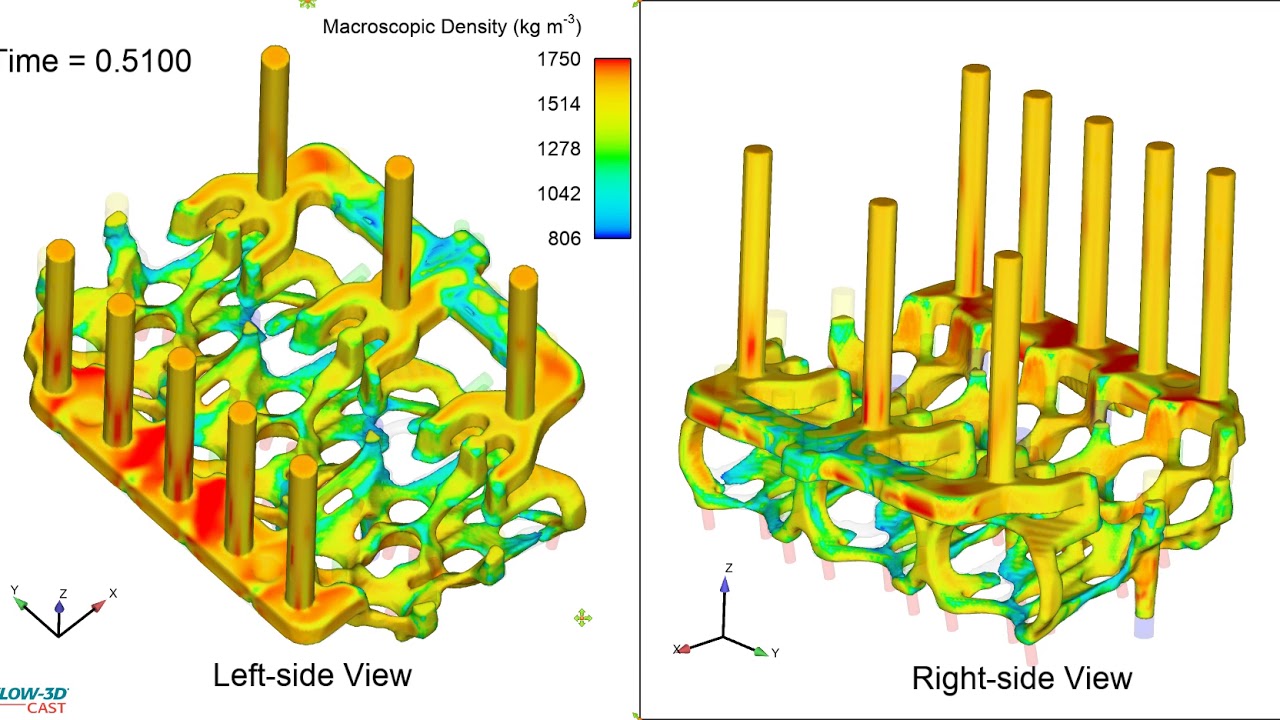
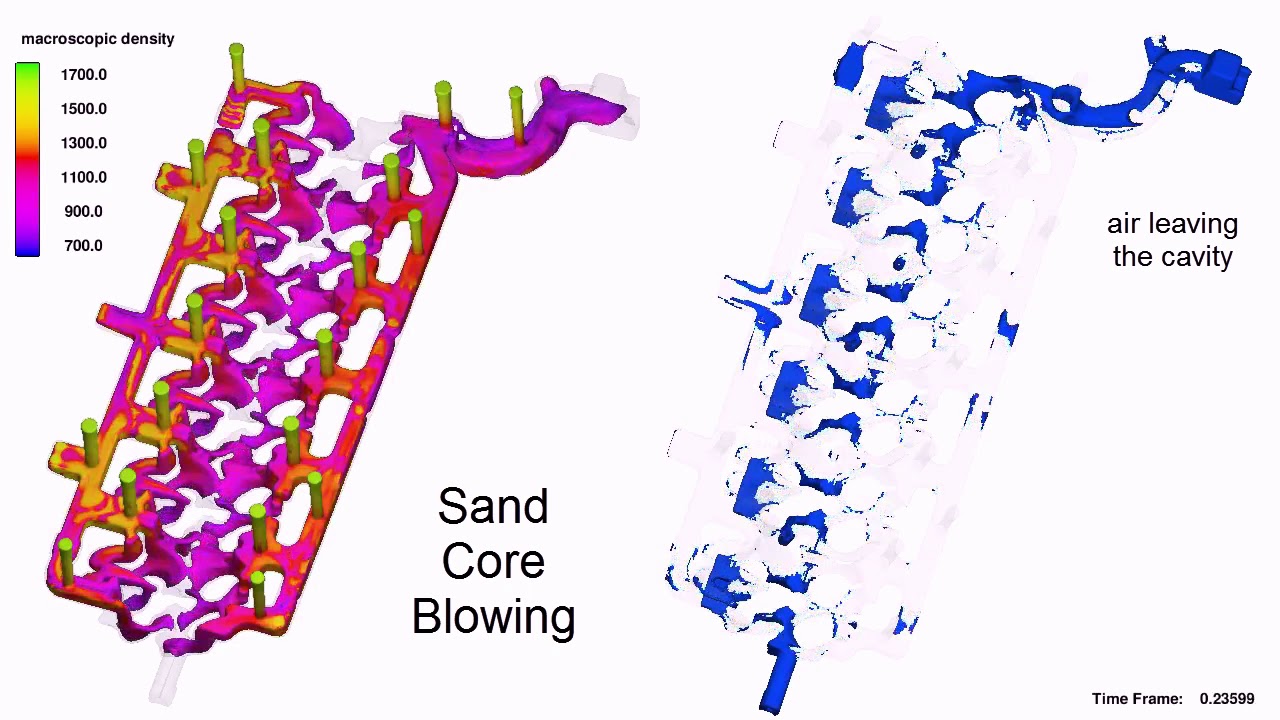
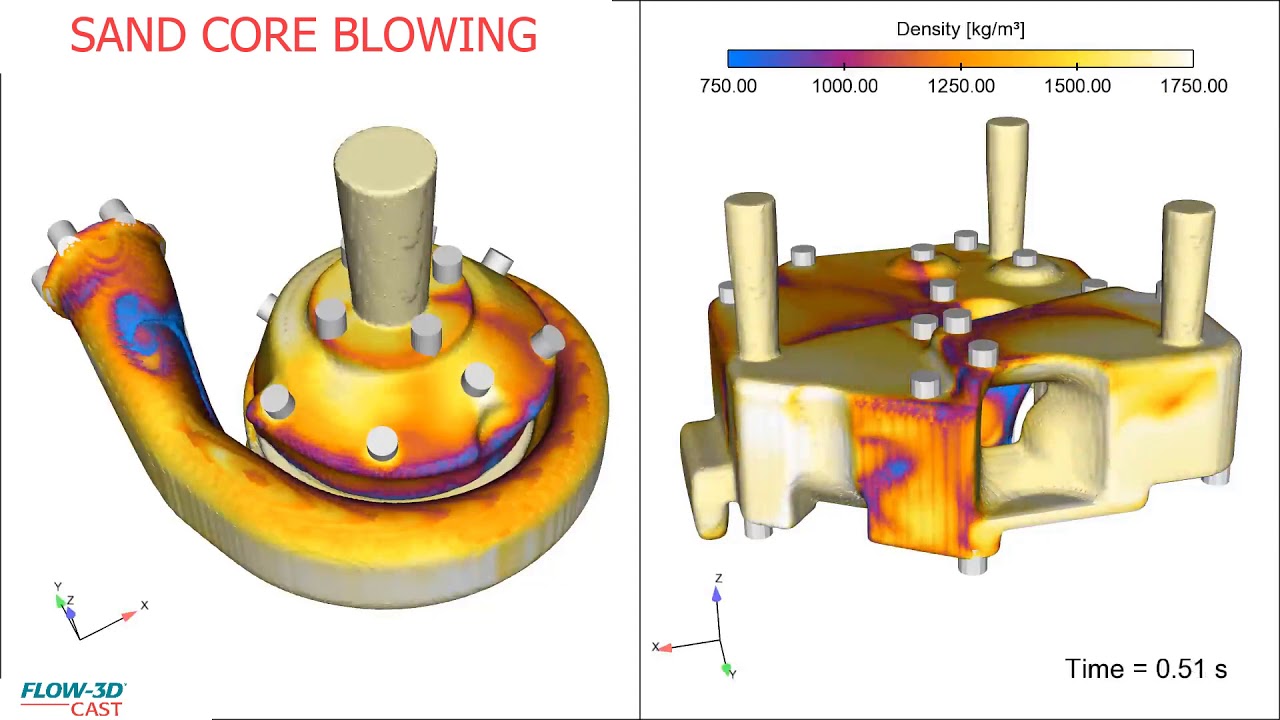
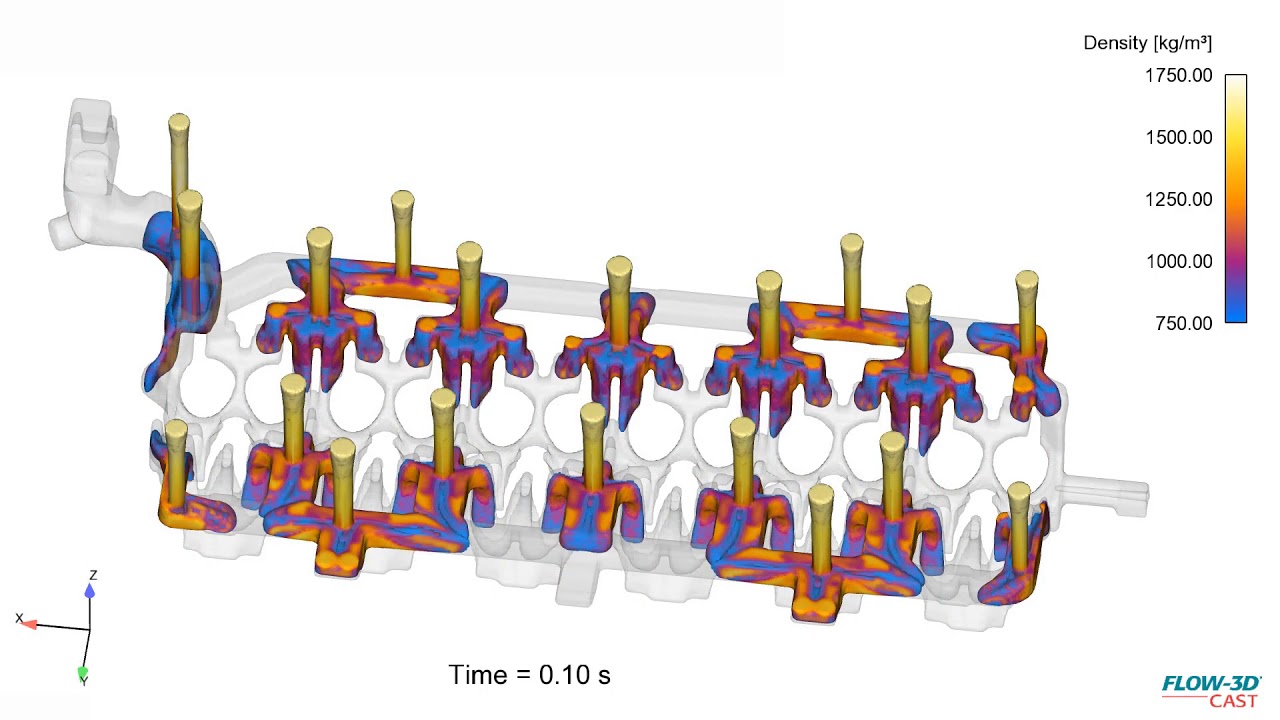
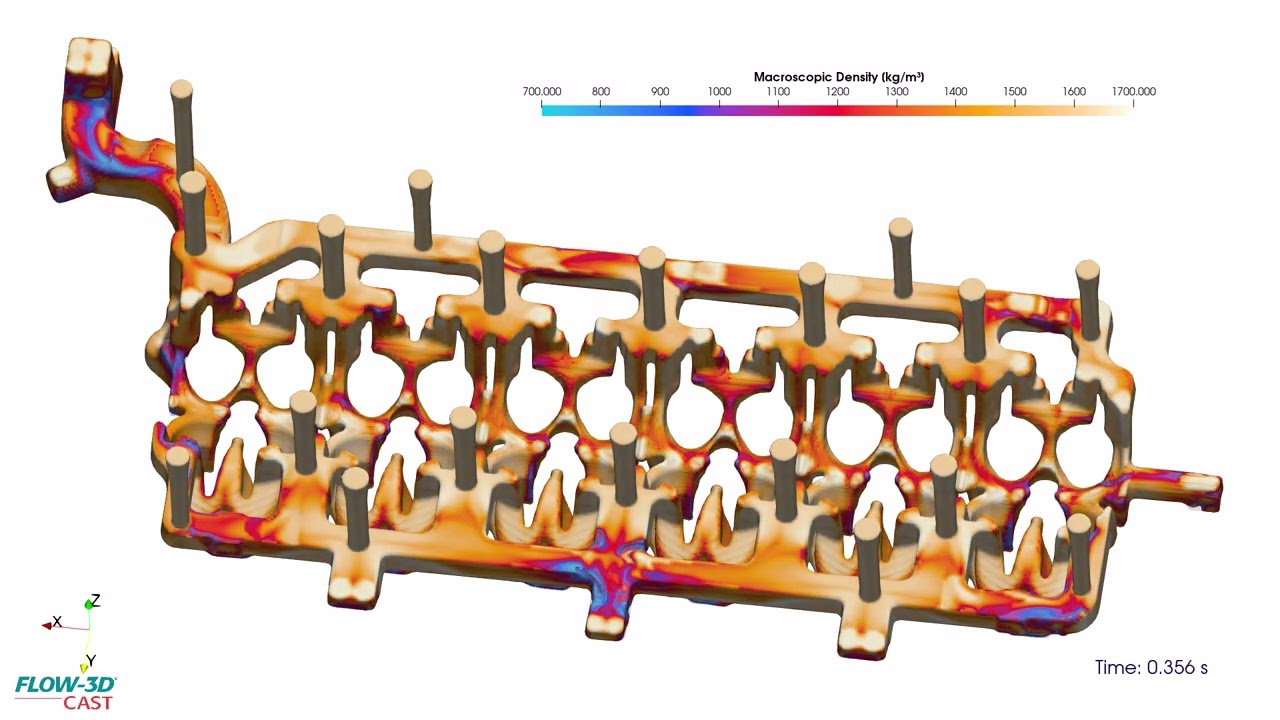
FLOW-3D CAST helps to establish robust process conditions and optimized solutions for sand core production including the shooting, gassing and curing of organic and inorganic binders for cold and heated core boxes. The animation shows the prediction of the filling patterns and sand packing densities during the shooting process. Based on these results, the number, dimensions, and positions of the shooting nozzles and core box vents can be optimized. By using FLOW-3D CAST to simulate this process, customers can produce flawless, high-quality sand cores.

Processes Modeled

Shooting

In the shooting process, a blow head filled with sand is pressurized with air, fluidizing the sand into a mixture of air, sand, and binder. This mixture flows from the blow head through shooting nozzles into the core box, forcing air out through venting nozzles. The goal is to achieve a sand density distribution in the core box that is as high and as uniform as possible. Process parameters that can be varied include shooting pressure and the number and position of shooting and venting nozzles, since it’s desirable to use as few nozzles as possible without sacrificing core quality.

Different configurations of shooting and venting nozzles and their impact on the resulting sand density distribution can be analyzed using simulation. Predicted velocities and shear stresses allow engineers to draw conclusions on the wear and lifetime of the core box.

Sand density distribution
Sand density distribution after the shooting

Gassing

In organic binder systems, sand is coated with an organic resin that hardens when exposed to a gaseous agent, usually amine, typically injected through the same nozzles used for shooting. Gassing must last long enough for the gas to reach every part of the core to ensure complete hardening, but not so long that it wastes the poisonous gas.

Simulation predicts the amine concentration distribution in the core over time, which corresponds to core hardness, allowing engineers to determine a sensible gassing time.

The simulation on the right predicts the amine concentration distribution in the core over time which is equivalent to the hardness of the core. This allows the engineers to decide on a sensible time-scale for the gassing process.

Amine concentration core
Amine concentration in a core

Drying

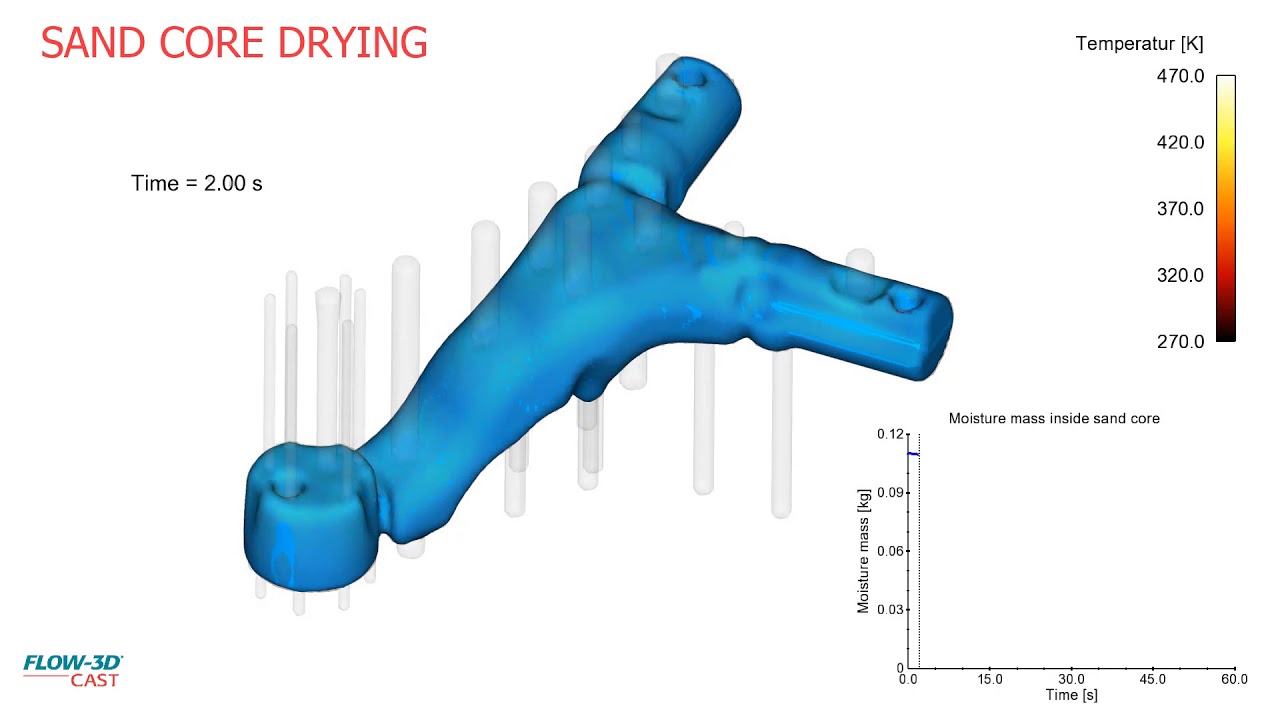
Inorganic, water-based binder systems are increasingly used in place of organic systems, offering an emission-free core production process and reduced core gas production during casting, which improves casting quality. For these binder systems, hardening requires removing water from the core, typically through the injection of hot air, and residual moisture becomes the measure of hardness. Simulation must model air flow through the core along with the evaporation and condensation of water and vapor and the transport of vapor with the hot air.

Sand core making validation
Correlation of predicted residual moisture and the damage of a real core

Tempering of core boxes

In certain core manufacturing processes, such as hot box and Croning, hardening occurs through a thermal reaction of the binder in a heated core box. The box is heated using heating channels and electrical heating elements, and a uniform temperature distribution is critical for good core quality. Simulation captures both convective and radiative heat transfer to predict the temperature distribution over time for a given heating element configuration, indicating both the uniformity of heating and the time required to reach the desired temperature.

Heated core box
Temperature distribution in a heated core box

Validation of the core blowing model

Experiments and simulations for a water jacket core

Core shooting experiments were carried out at TU Munich’s Foundry Institute. Process parameters such as shooting time and pressure, and the number of inlets and vents, were varied and their influence on core quality analyzed. The occurrence of defects in the real cores correlated well with the areas of low sand density predicted by simulation.

Core blowing validation
Core defects compared to simulated density distribution
Casting defects of a rear axle housing
Validation surface defects
Correlation of surface defects and simulated density distribution

Request More Information

Please select a valid form