

Sand Casting Playlist
1:25
0:18
0:18
0:07
0:43
0:10

0:22
1:10
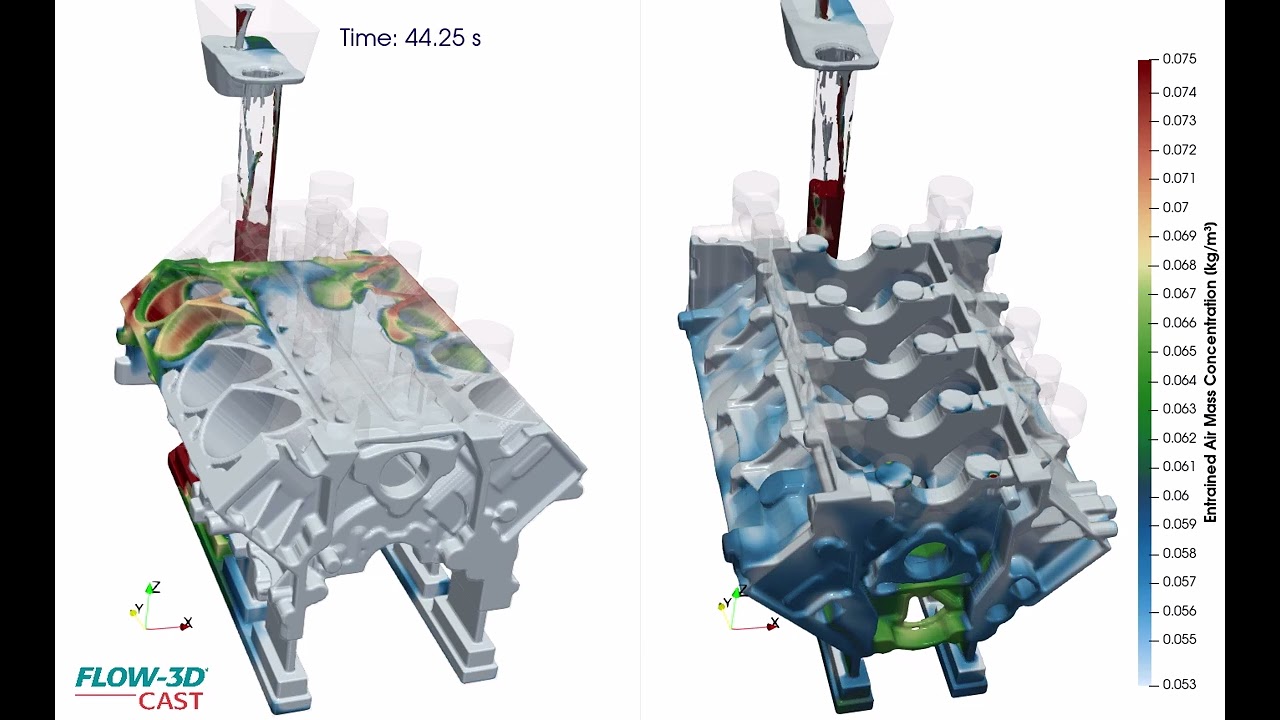
This simulated entrained air filling is a comparison of the casting with engine cylinders oriented up and down. The key observation here is that entrained air (gas porosity) collects towards the end of runner and backfills into the casting in addition to significant recirculation of air. Further, the sprue flow shows additional air building and transferring into the casting later in fill. While the orientation of cylinders downward helps in reducing the highest concentration of air in comparison to the cylinders up, the sprue and runner design leaves room for improvement.
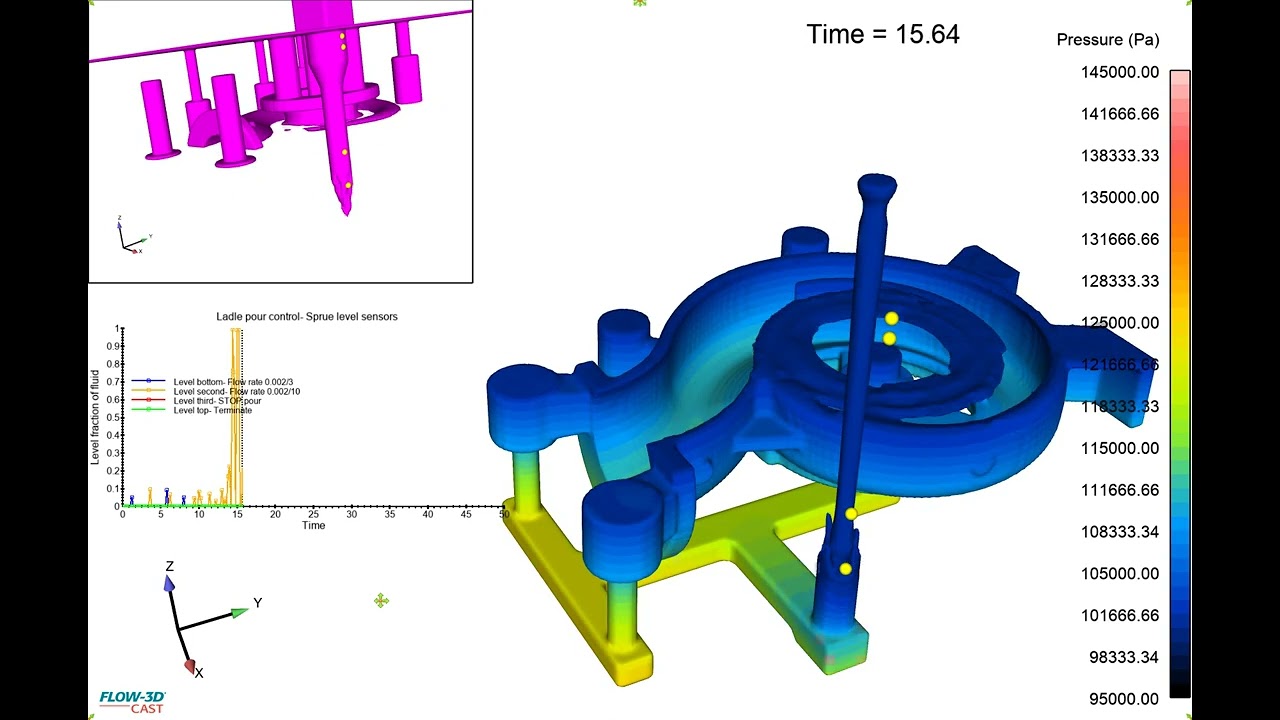
A flow simulation is best correlated with an identical pouring control as in a foundry and with similar fill time. Shown here is a FLOW-3D CAST simulation with sprue level sensors varying rate of pour to retain a head pressure and level in the sprue, as in a foundry while hand pouring. Additionally, the view of air in the cavity helps identify bubbles being entrained during pour.
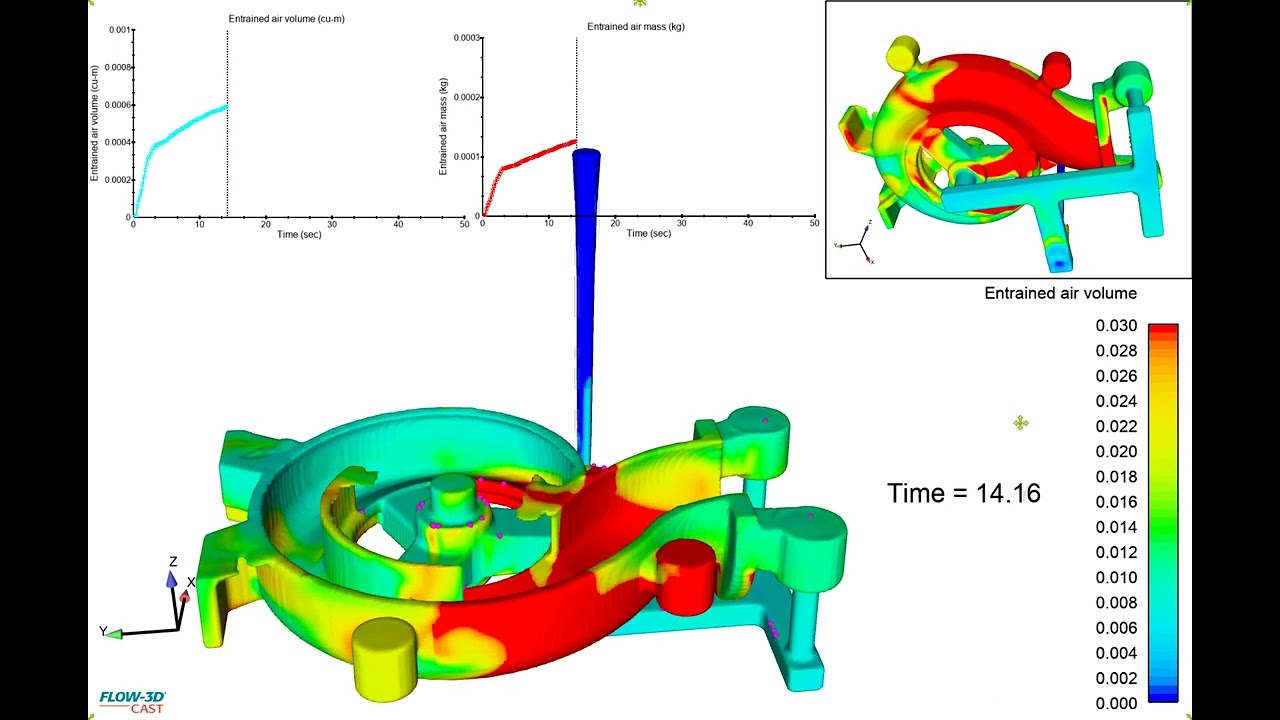
Gas porosity in steel casting castings can be analyzed using simulations of mold filling with entrained air mass or volume. Shown here is a simulation of entrained air volume with plots quantifying mass and volume of entrained air in metal vs. time. The particles represent any collapsed bubbles that are likely to show gas porosity within the casting.
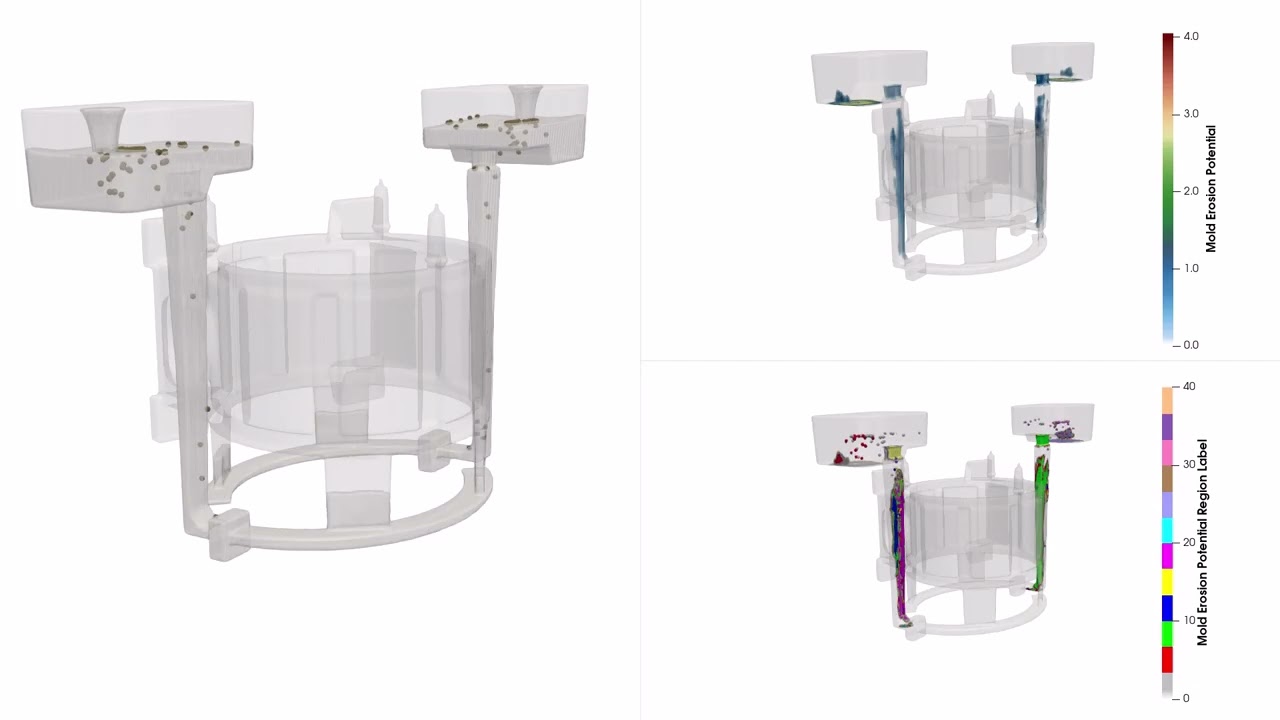
This FLOW-3D CAST video demonstrates the mold erosion calculation and sand inclusions generation/tracking for a gravity sand casting. Sand inclusions are generated at high mold erosion potential regions, where the mold will likely be damaged due to long exposure to high-velocity metal flow. However, the sand inclusions generated in the pouring basin and on the down sprue surface are eliminated by the filter at the bottom, and thus will not go into the casting. The sand inclusions generated in the runner after the filter may end up in the casting depending on the metal flow. The sand inclusions are marked by the mold erosion potential region label, which can be used to trace their origins.
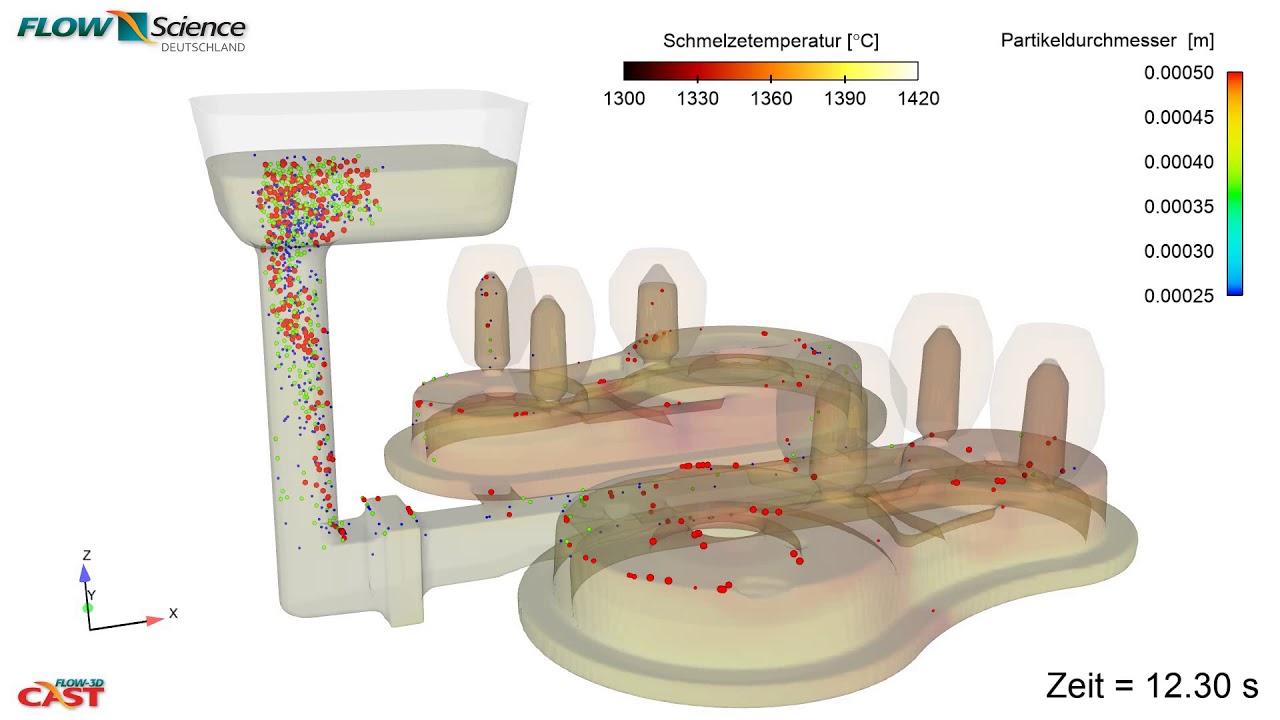
The simulation demonstrates the use of the particle model in FLOW-3D CAST to track the entrainment of air bubbles during the filling of a sand casting part.
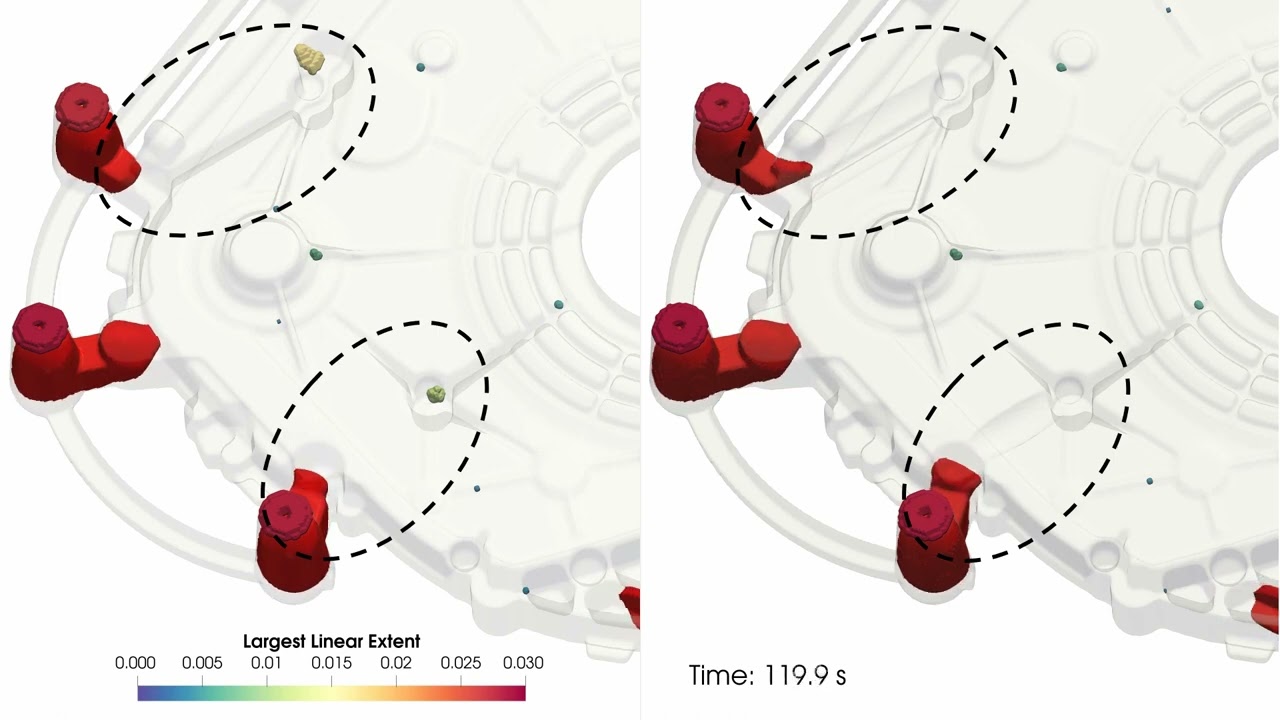
This FLOW-3D CAST simulation shows large porosities in the initial version on the left side due to large hot spots within the casting where solidification-induced shrinkage creates a deficit. In the optimized version on the right, the melt solidifies in the direction of the risers. This means that the deficit can be compensated by the riser and no porosity is created in the casting. Learn more at https://www.flow3d.com/optimization-of-a-sand-casting/
This FLOW-3D CAST filling simulation of a turbo housing is used to understand oxide formation in the metal front.
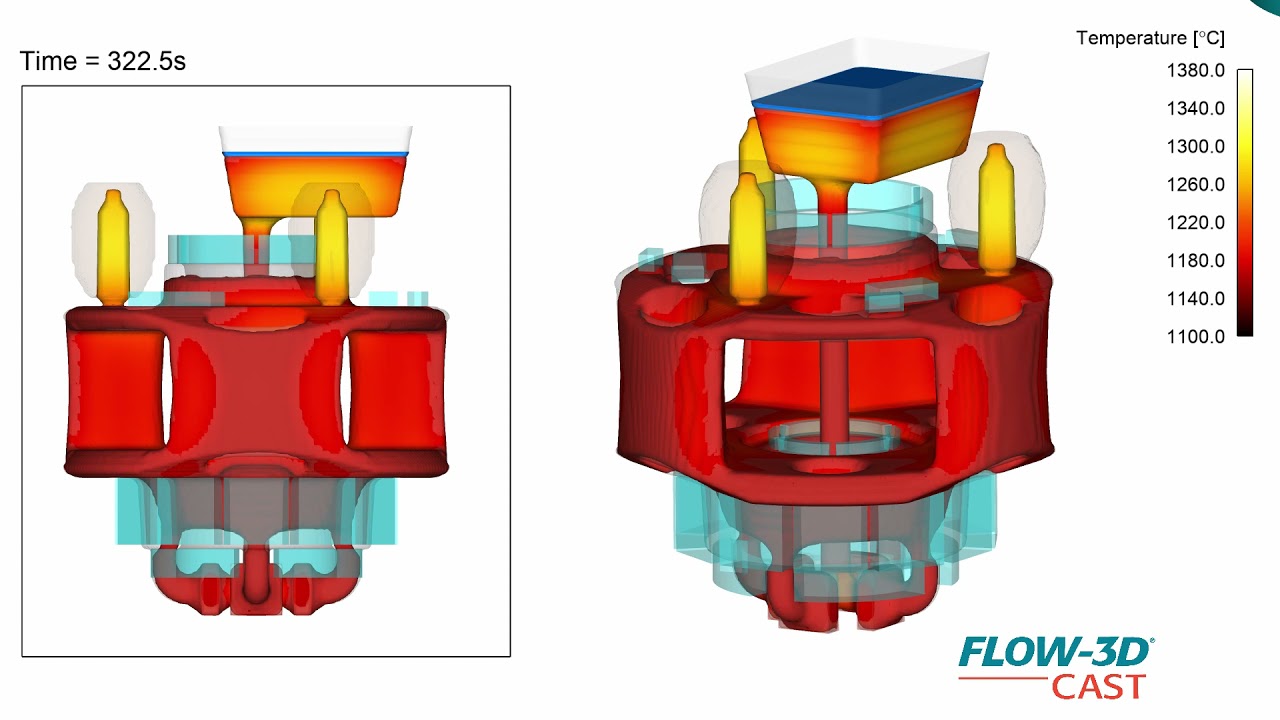
This simulation shows the filling of a planetary carrier with a ladle. The complete process from filling to solidification can be simulated with FLOW-3D CAST, including chills and exothermic risers, allowing for accurate prediction of casting defects and ensuring the best possible casting design.