

High Pressure Die Casting Playlist
0:10
0:11
0:13
0:21
0:17
0:08
0:17
0:51
0:18
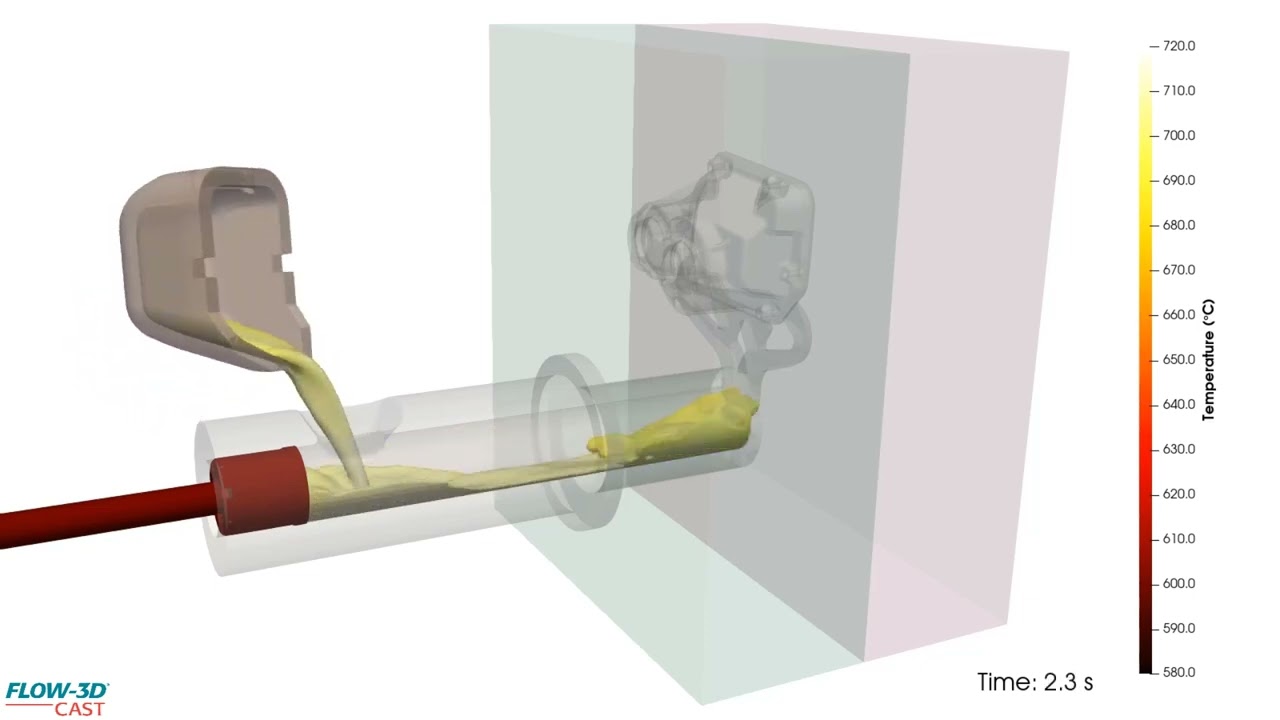
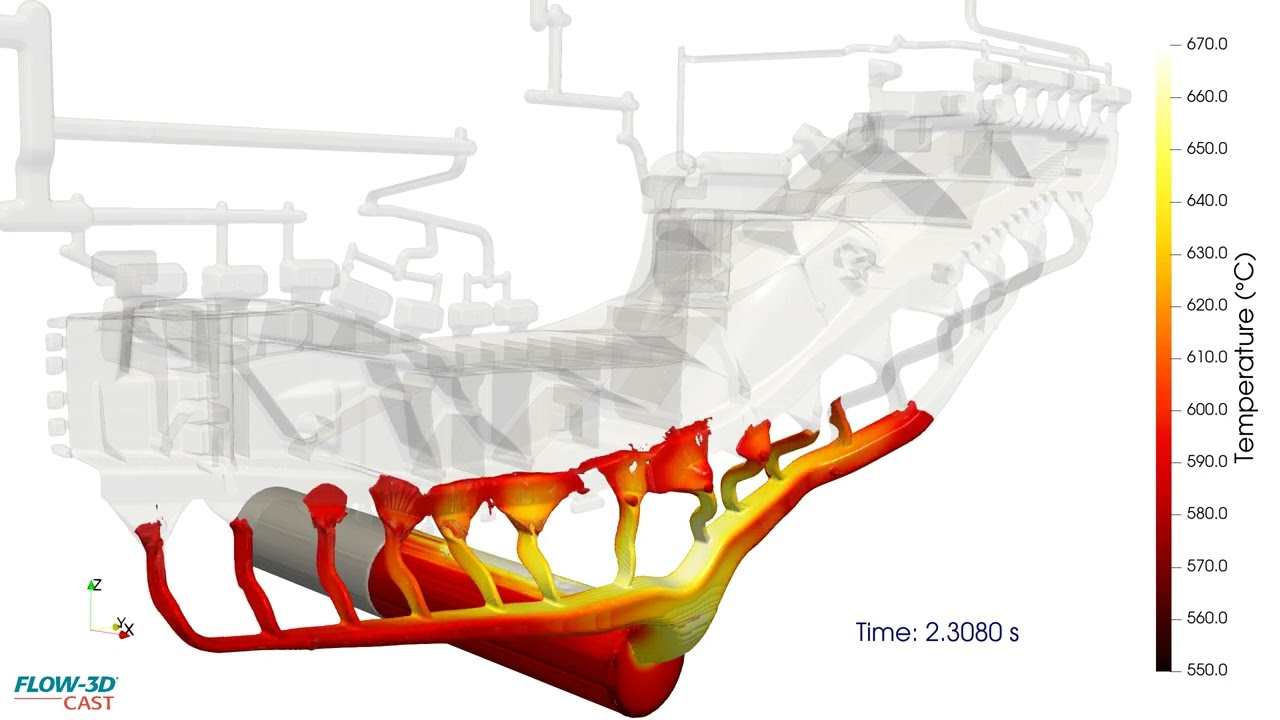
FLOW-3D CAST is used to accurately simulate the complex process of pouring into a shot sleeve using a ladle. Here, the thermal contours indicate pouring temperature vs. thermal loss in the dosing process. The wave propagation within the shot sleeve is accurately captured with the momentum transfer from pouring through ladle spout and the back fill from biscuit. This is crucial in computing the thermal loss and movement within the shot sleeve before the plunger pushes the metal into the casting. The heat generated in the shot sleeve can also be evaluated depending on duration of dosing and slow shot in tooling design for heating or cooling lines, thereby managing optimal thermal energy.
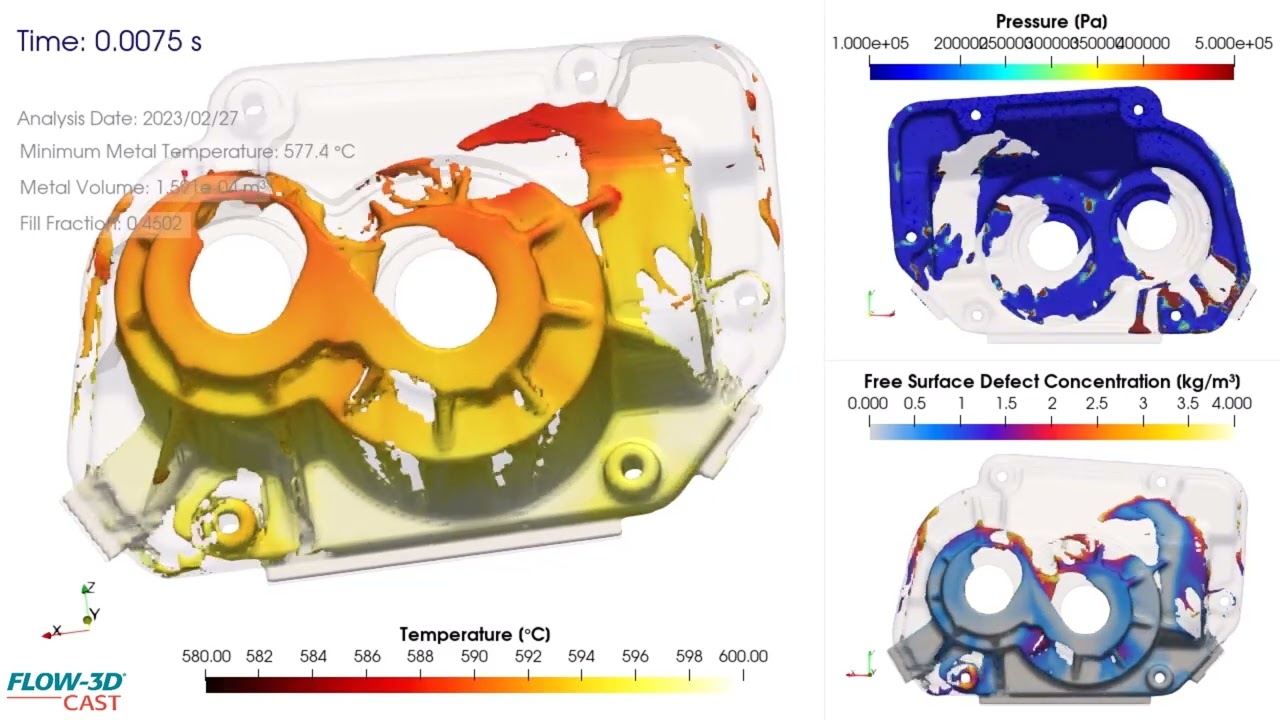
This high pressure die casting simulation shows filling of an aluminum alloy casting. FLOW-3D CAST is used to calculate the complex filling of a thin part and separation of the metal front as it climbs the two boss features in the casting geometry. The thermal contours indicate a 20degC drop in temperature between flow through ingates and complete fill of casting (without overflows). The illustrated free surface defect oxide contours identify areas where overflows can be added to remove oxides trapped in the metal. The animation showing pressure of gas trapped in the casting cavity is useful to see pressurization and last regions to fill, indicating the need for overflow vents to avoid gas porosity.
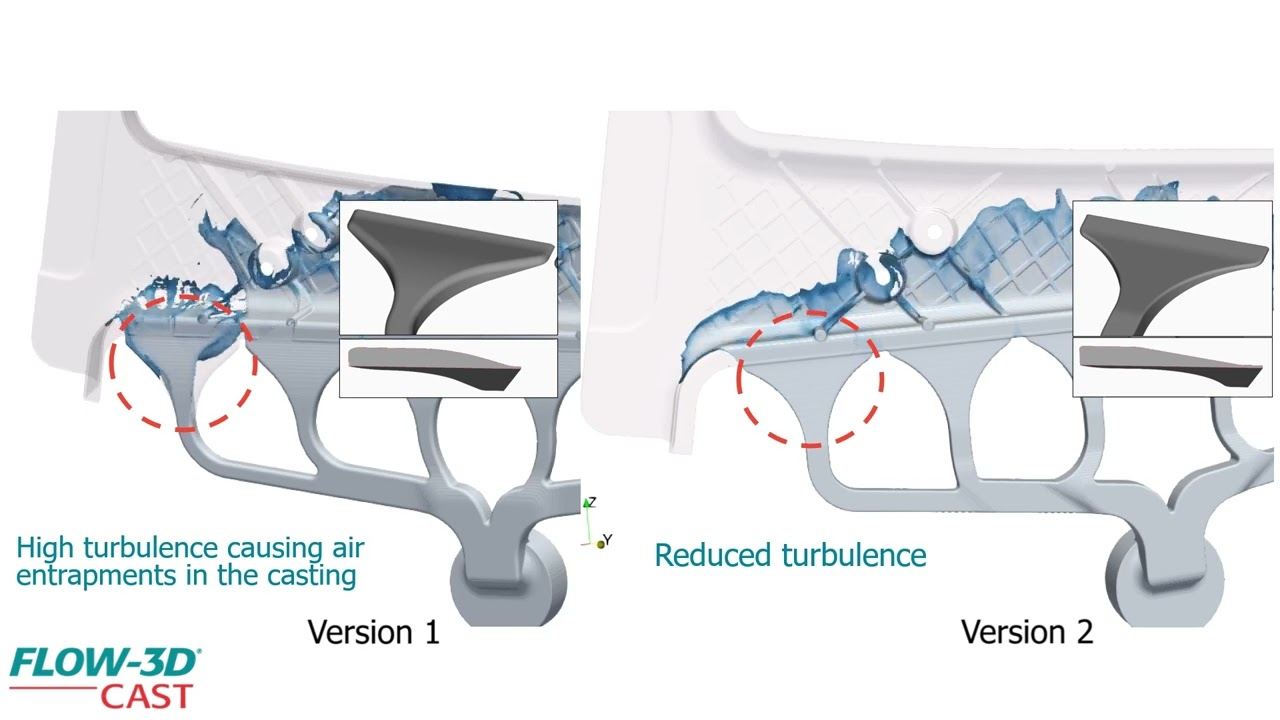
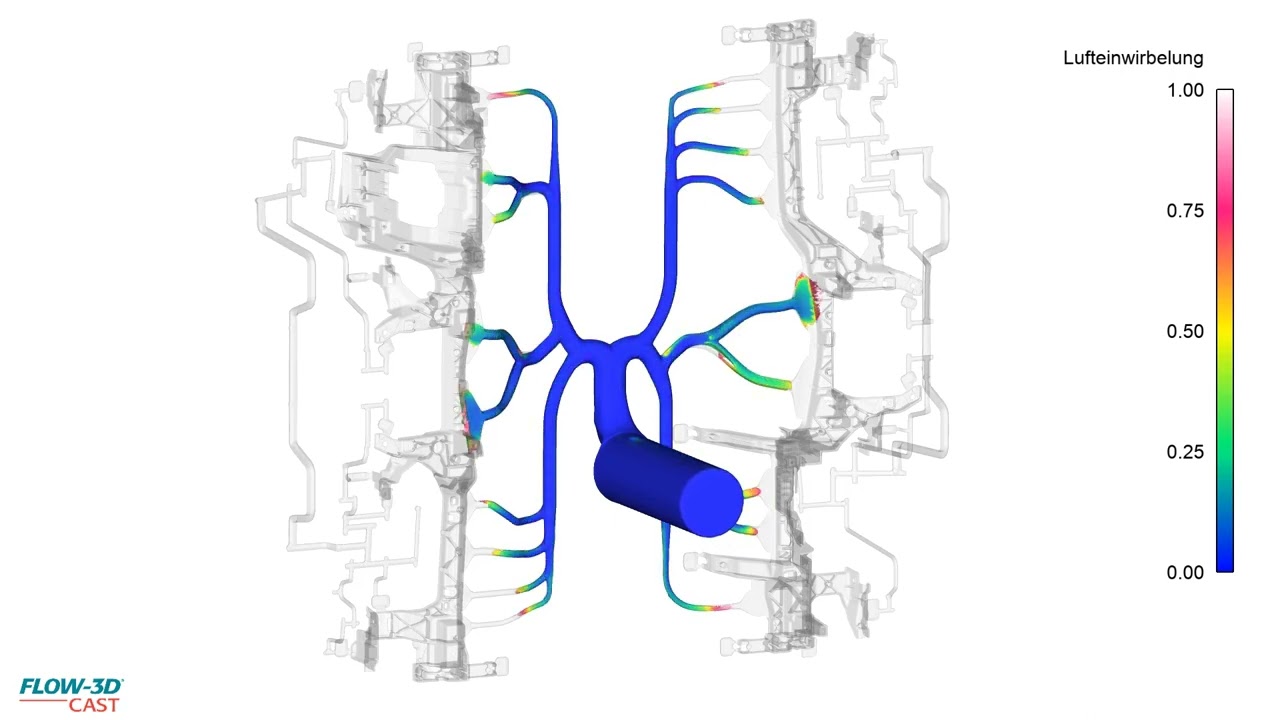
The correct ingate shape has a huge influence on ultimate casting quality. Here, the cross-section of the ingate system along the metal flow plays a big role. In version 1, the cross-section is increased in a critical area, leading to air entrapment and high turbulence, which also occur in the casting part itself. Version 2 shows a slightly decreasing cross-section along the melt flow. This reduces turbulence and enables a seamless melt front in the casting part. Read the full case study at https://www.flow3d.com/hpdc-system-optimization-and-cost-reduction/
FLOW-3D CAST offers a unique combination of accurate flow simulations, defect detection, optimization capabilities and support for large, complex castings, making it the ideal choice for the simulation of HPDC structural components. The modeling of the mold filling through the realistic movement of the plunger provides exact results of the melt temperature. This enables associated problems, such as cold running, to be predicted precisely.
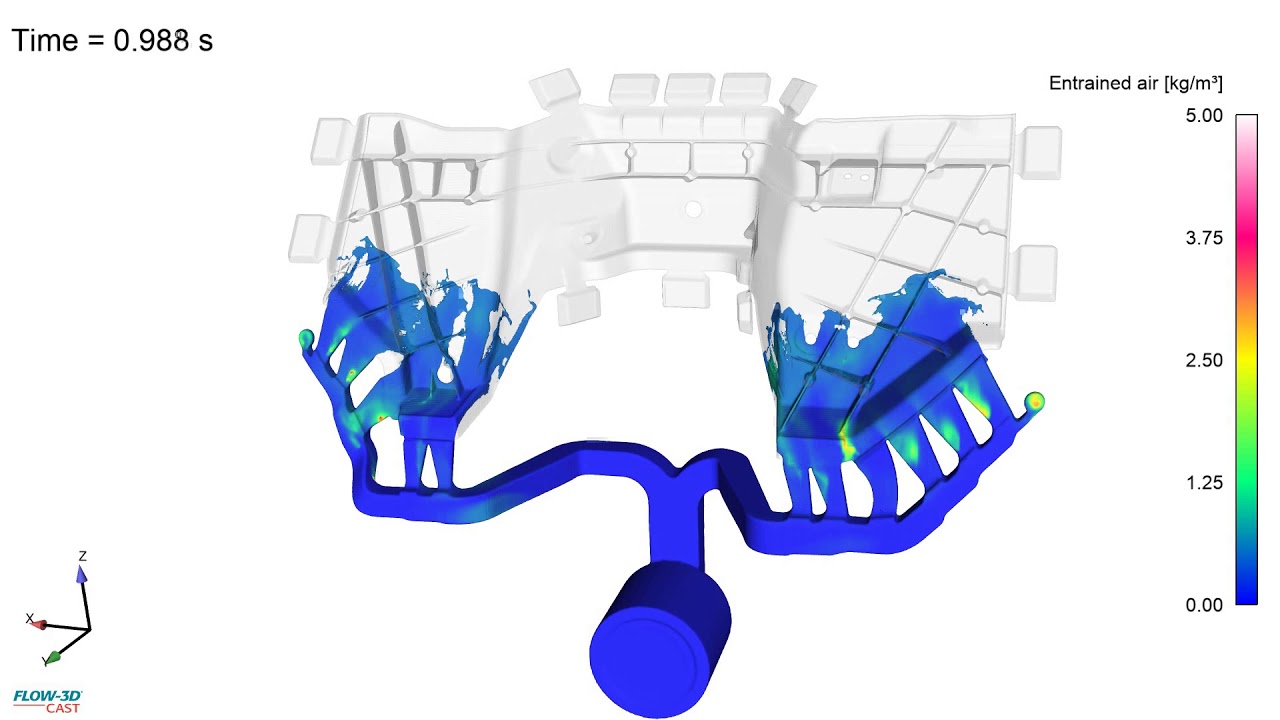
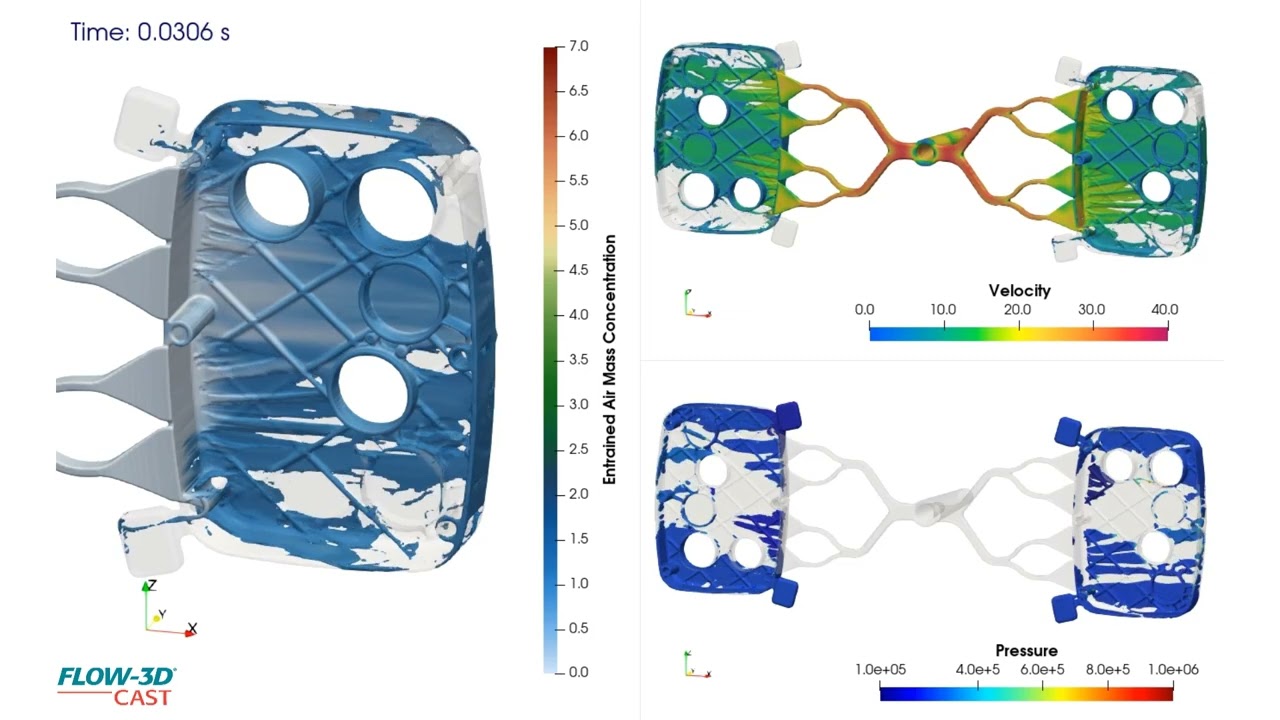
This FLOW-3D CAST simulation is a two-cavity high pressure die casting filling for an automotive instrument panel. The color shows air entrained in the metal as it violently moves through the cavity. Note that the movement of the piston in the slow stage of the filling is suboptimal since it traps a volume of air that is then pushed into the cavity.
This FLOW-3D CAST filling simulation of a complex thin walled part shows the air entrainment variable to understand where defects can become an issue in the filling process. Visualization of air entrainment can be used to understand die venting, back-pressure, and areas of porosity.
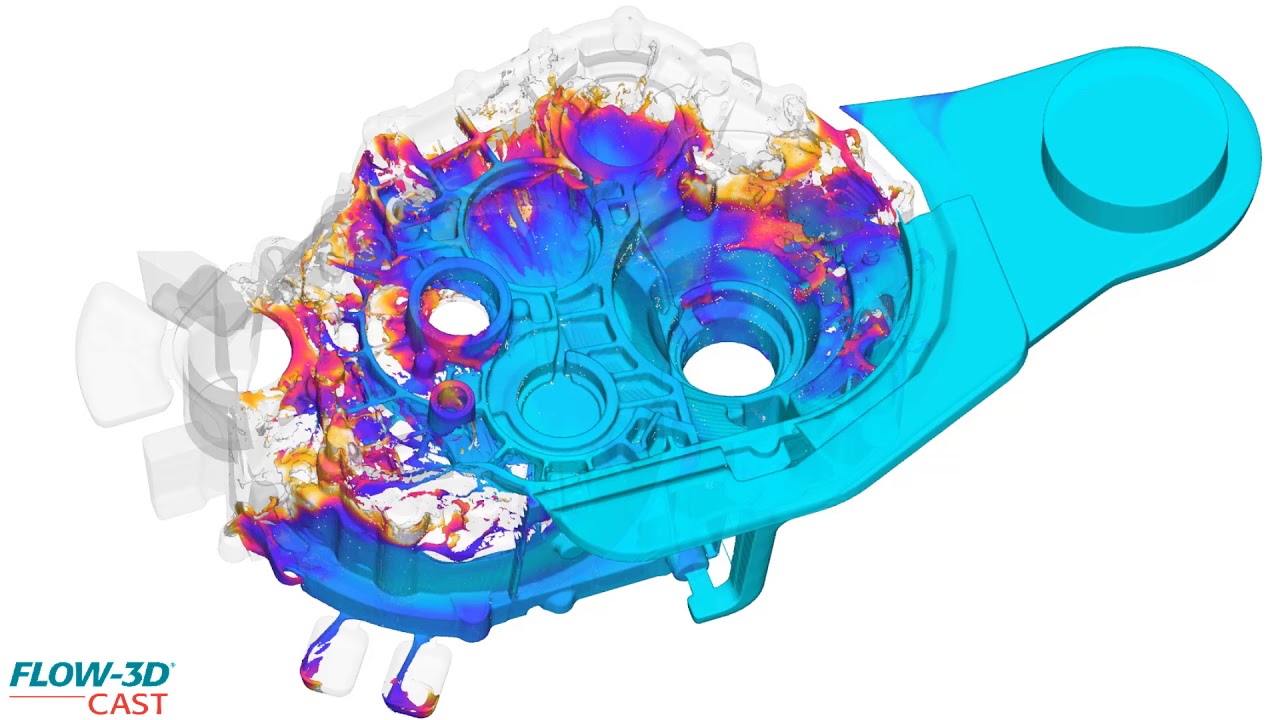
FLOW-3D CAST‘s defect tracking capabilities help casting engineers predict where surface oxide defects are most likely to occur from the filling process. Oxides form due to an exposed molten metal surface to air and can end up in the part in undesirable locations. The final location of the defects depends on the overall flow conditions, turbulent mixing, fluid jetting and impingement. FLOW-3D CAST accurately tracks these oxides and their final locations to help improve designs.
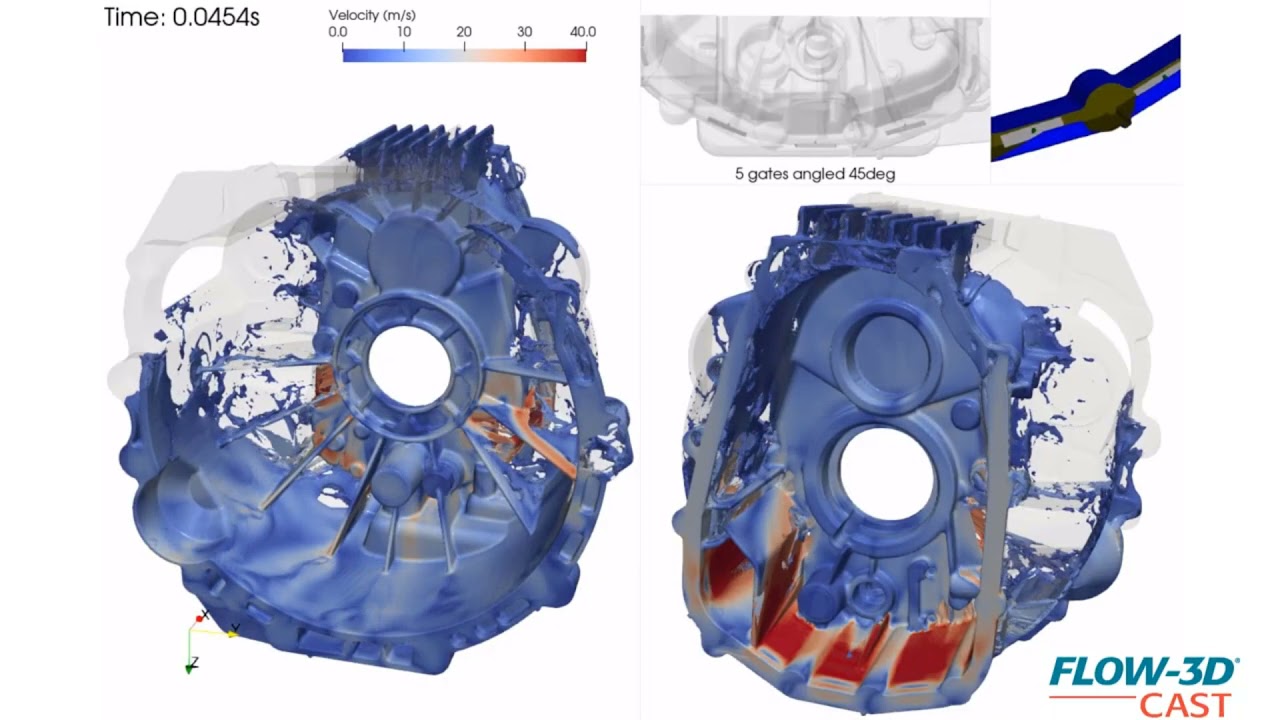
This is a simulation of an automotive flywheel or bell housing, showing velocity contours of an aluminum alloy during a fast shot of a high pressure die casting process. It is part of a design phase to evaluate different gating options. In this simulation, gates are angled at 45 degrees. The comparison between this and other gate angles helps visualize the effect of gates on this highly turbulent fill before addressing runner designs.
The solidification process of hot chamber HPDC is simulated using FLOW-3D CAST. Filling behavior and small droplets (splashes) must be considered to represent this process. A special particle model is used to reduce the computation time. If a droplet occupies a very small portion of the mesh cell, it is converted to a particle. Tracking of its movement is much less computationally expensive in this case. Velocity during the filling process is analyzed to confirm proper gate design. It proves that the critical velocities of 50 mm/s are not achieved during the process. Recent additions of an even more physically detailed air entrainment model allow entrained air, which is assumed to be in the form of bubbles, to be modeled as rising in the surrounding liquid metal because of buoyancy forces and even leaving the liquid if it reaches a free surface.